How to Choose a Roof Sheet Roll Forming Machine 2026?
Choosing the right Roof Sheet Roll Forming Machine is a practical decision, not a simple equipment purchase. The machine must match your products, materials, workshop space, and production targets. A glossy brochure can hide important limitations.
Begin with the roof sheet profile you plan to manufacture. Trapezoidal panels, corrugated sheets, and tile-effect profiles require different roller designs. Check the compatible material thickness, coil width, yield strength, and coating type. A machine designed for thin galvanized steel may struggle with heavier or painted coils.
Production speed also needs careful attention. High speed sounds attractive, but unstable feeding can create scratches, uneven lengths, or poor profile accuracy. Inspect the decoiler, forming stations, cutting system, electrical controls, and emergency protection. Ask for sample sheets, dimensional records, and a live production test.
Experience matters here. An experienced supplier should explain how tooling affects service life and maintenance. They should also provide clear installation guidance, spare-parts support, and operator training. Reliable technical documents are more valuable than exaggerated promises.
There is no perfect machine.
Your real challenge is balancing output, quality, budget, and future expansion. A lower purchase price may bring higher maintenance costs later. However, the most expensive option is not automatically the best choice. Consider local power conditions, available technicians, factory layout, and expected coil consumption. Leave enough space for loading and safe sheet handling.
Before signing a contract, compare several suppliers using the same specifications. Record their answers. Recheck every assumption. Small details often decide whether your Roof Sheet Roll Forming Machine becomes a dependable production asset or an expensive disappointment.
What Is a Roof Sheet Roll Forming Machine?
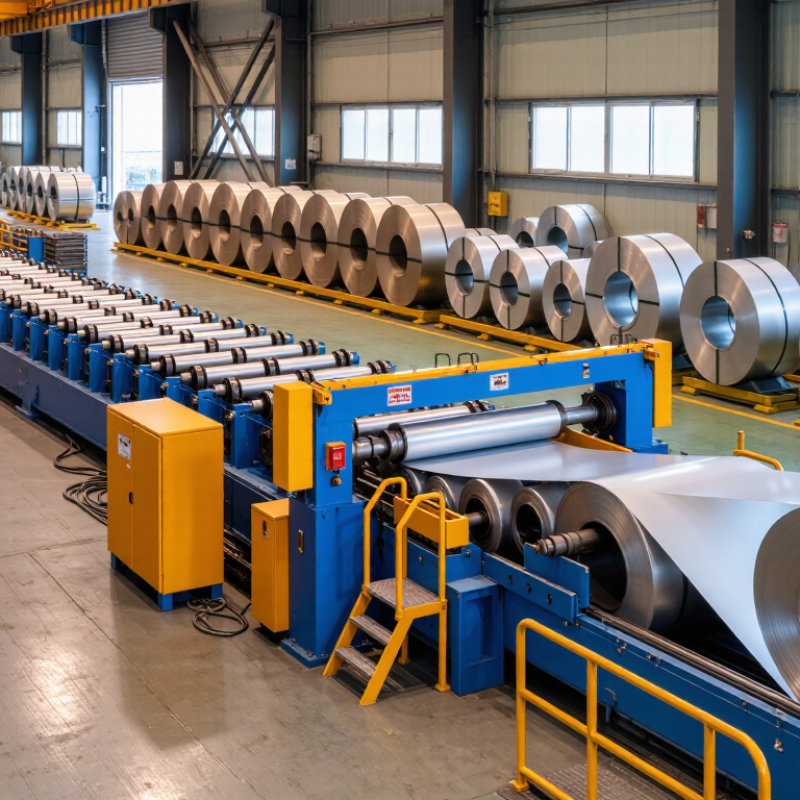
A roof sheet roll forming machine converts coiled metal strip into continuous roofing panels. The strip passes through several shaped rollers, each making a small bend. The final profile appears gradually, not in one sudden press. A cutting unit then separates panels at programmed lengths. Most systems include an uncoiler, leveling section, roll forming stations, hydraulic cutter, and control cabinet.
The process suits galvanized steel, coated steel, and aluminum sheets. Material thickness often ranges from 0.3 to 0.8 millimeters, depending on the roof profile and engineering requirements. World Steel Association data placed global finished steel demand near 1.75 billion tonnes in 2024. This scale shows why stable forming equipment matters for construction supply chains. However, steel demand alone does not determine machine quality.
In practical inspections, I check roller alignment, shaft rigidity, cutter accuracy, and emergency stopping performance. A machine can be technically correct and still produce uneven ribs. That problem is easy to miss during a short factory demonstration. Production speed also needs careful review. The stated speed may exclude cutting, coil changes, and adjustments. According to the International Energy Agency’s Energy Efficiency 2024 analysis, industrial efficiency depends heavily on reducing process losses. Therefore, a suitable 2026 machine should minimize scrap, setup time, and profile distortion. I would request test panels using the buyer’s actual material before approval. This step takes time. It can prevent expensive misunderstandings.
How to Choose a Roof Sheet Roll Forming Machine in 2026?
What Is a Roof Sheet Roll Forming Machine? Compare typical material thickness capability and production speed for common roof sheet profiles before selecting a machine.
These representative industry ranges show that heavier or more complex profiles usually require greater thickness capacity and may operate at a lower forming speed. Confirm the required sheet thickness, coil width, profile depth, forming stations, automation level, and cutting accuracy with the machine supplier before purchasing.
Which Roof Sheet Materials and Profiles Does It Support?
When choosing a roof sheet roll forming machine in 2026, start with the material, not the advertised speed. Galvanized steel is widely used for corrugated and trapezoidal roofing. Prepainted steel also performs well, but its coating can scratch during forming. Aluminum requires careful tension control because it bends more easily. Stainless steel is stronger and may need heavier tooling and slower production. Material thickness, yield strength, coil width, and coating type must match the machine design.
Profile selection is equally important. Common options include corrugated sheets, trapezoidal panels, tile-shaped sheets, and standing seam systems. Each profile needs dedicated rollers, cutting settings, and forming passes. A machine designed for one profile may produce another, but the result can show waves, cracked edges, or inaccurate overlaps. That matters. Ask for actual profile drawings, not only sample photographs. Check the effective cover width, rib height, pitch, and allowable thickness range.
In practical inspections, I measure the finished sheet after several production cycles. Small deviations often appear when the coil temperature, leveling, or guide alignment changes. Operators should test the first sheets and inspect the edges, coating, hole position, and cut length. Some suppliers describe a machine as “universal,” yet tooling changes may be slow or limited. I have seen buyers overlook this detail. A reliable choice includes documented tolerances, clear adjustment procedures, and suitable spare rollers. The machine should support your planned materials and profiles, not an ideal list that cannot be verified.
How to Compare Costs, Suppliers, Installation, and After-Sales Support
How to Choose a Roof Sheet Roll Forming Machine 2026?
Machine price is only the visible part of the investment. Compare total cost, including decoiler capacity, tooling, electrical components, freight, commissioning, training, and spare rollers. The World Steel Association reported 1.89 billion tonnes of crude steel production in 2023. Material availability remains important, but stable production depends more on machine control and maintenance. Request a cost breakdown for your actual coil width, thickness, speed, and profile. A low quote may exclude installation or software support.
Tips: Ask for three comparable quotations. Check warranty terms, response times, spare-part stock, and customer references. Require a test run using your own galvanized coil. Record profile tolerance, line speed, noise, and changeover time. Small details matter.
Installation can affect output for weeks. Confirm foundation requirements, power load, leveling tolerances, and operator training before shipment. Deloitte’s 2024 Smart Manufacturing Survey found that 86% of manufacturing leaders expect smart manufacturing to become a major competitiveness factor within three years. That supports choosing reliable controls, but advanced functions are not automatically valuable. Some factories pay for automation they rarely use. I would challenge that decision. After-sales support should include remote diagnostics, service manuals, preventive-maintenance schedules, and defined escalation contacts. Ask how quickly worn bearings, sensors, or forming rollers can be supplied. A supplier’s promises are useful; documented response records are better.